Skip to content
Siropol

High-temperature polymer injection moulding

Demanding polymers,repeatable parts

We process PEEK, LCP, PPS, PA, and technical and high-temperature polymers in which we specialise. More than 30 injection moulding machines, an in-house toolroom and a metrology laboratory at one location.

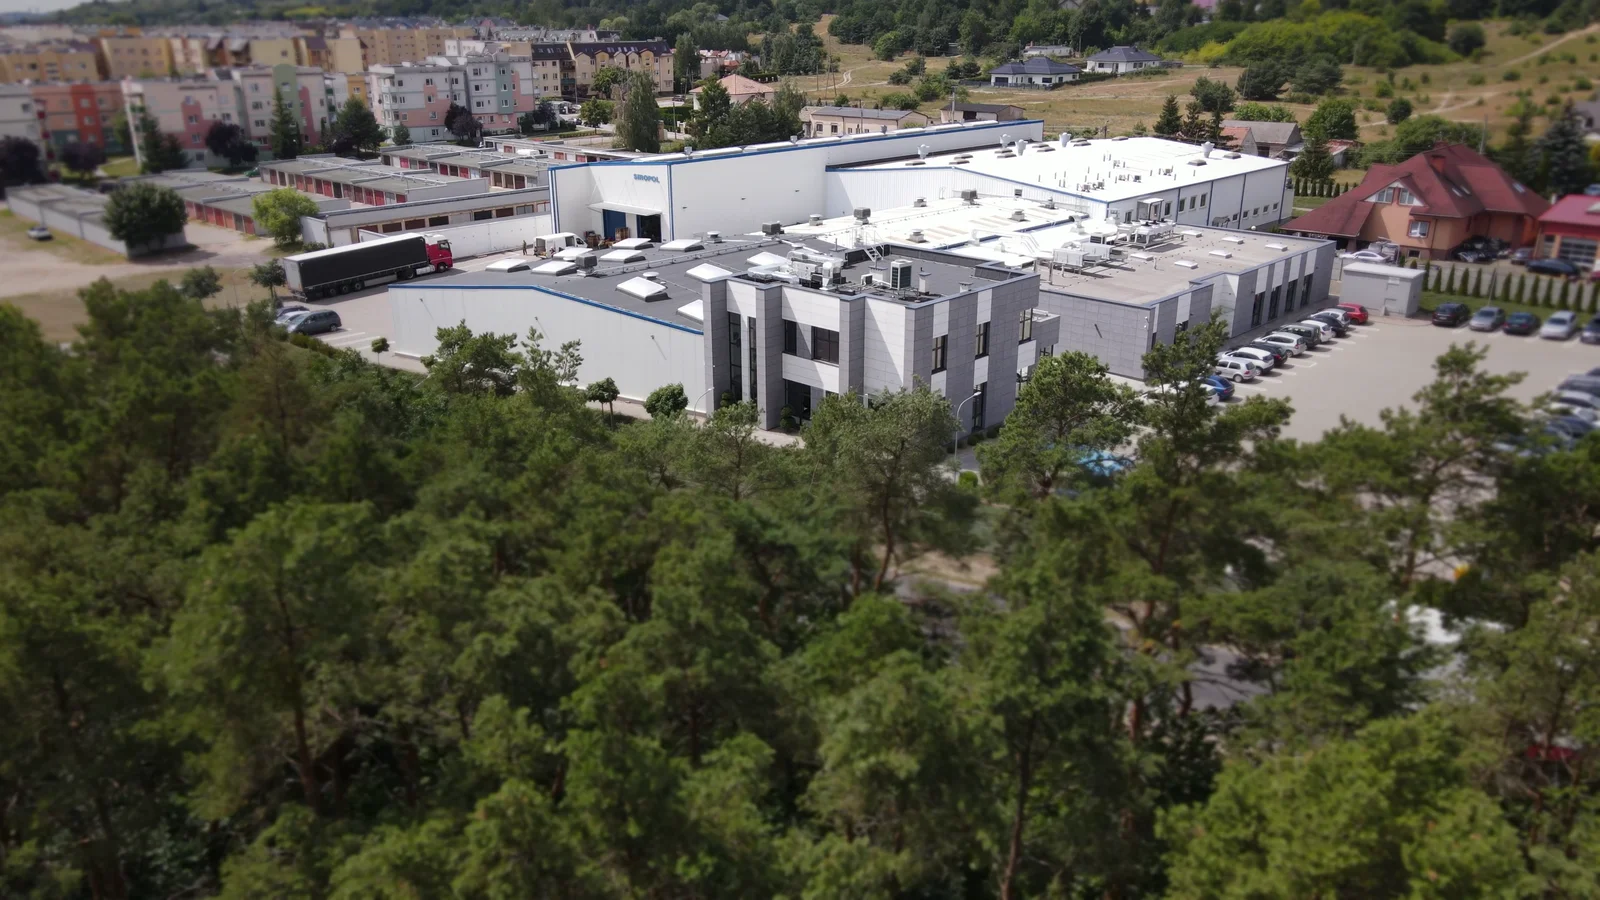
Bydgoszcz, Poland
53.17°N · 18.16°E
Siropol

Born to mold

  • 30+

    Injection moulding machines

  • 1000+

    Active part numbers

  • 100+

    Employees

  • 30+ yrs

    Experience since 1996

  • IATF16949

    Automotive certified

01

High-performance polymers

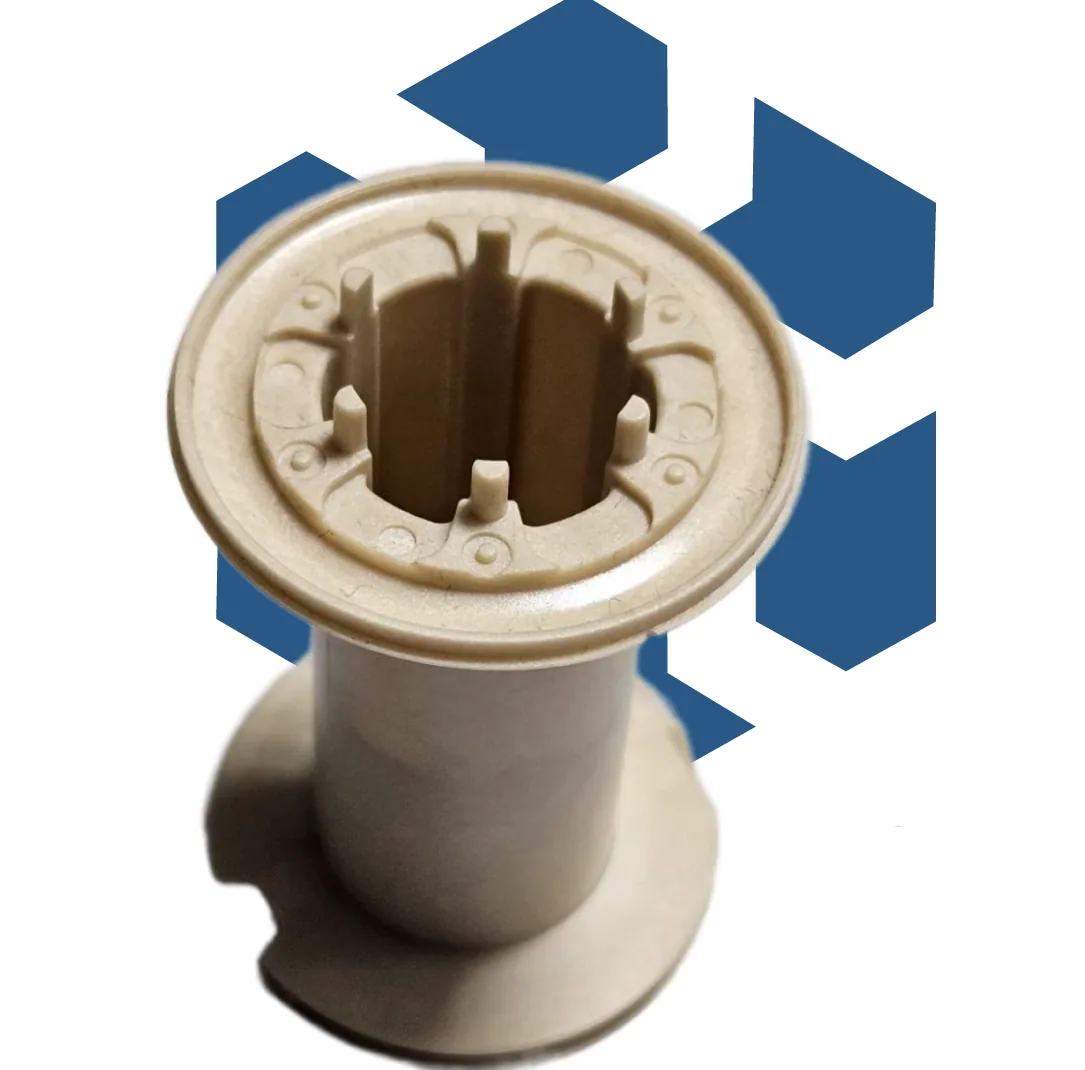
This is our advantage. Few injection moulders in Central Europe manufacture parts from all three polymers—PEEK, LCP and PPS—in series. Each polymer requires specific processing conditions, a suitably designed mould and specialist expertise.

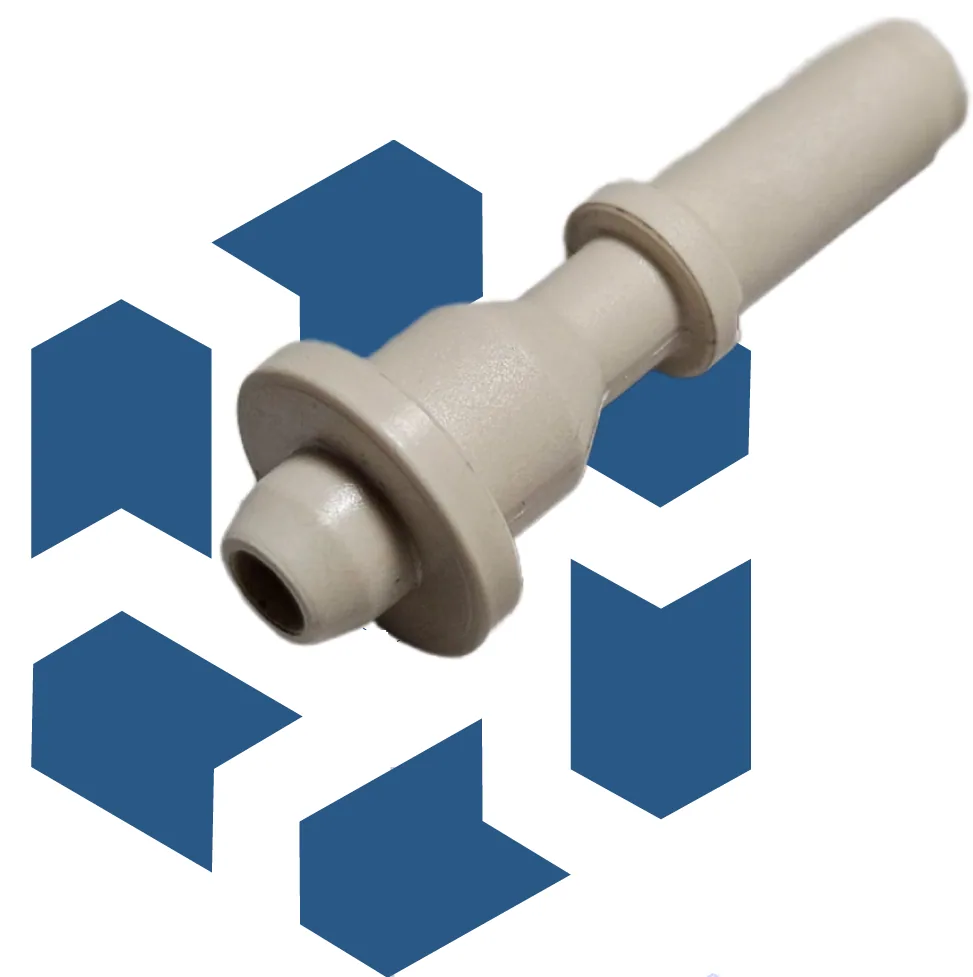
PEEK injection-moulded part

PEEK

Polyetheretherketone

Continuous service temp.

to 250 °C

Replaces metal where mass and chemistry both matter.

Advantages

  • Outstanding thermal stability and creep resistance
  • Hydrolysis resistant, stable against aggressive media
  • Excellent tribological and fatigue behaviour

Processing challenge

A 360–400 °C melt and an oil-heated tool at 170–200 °C. Requires a dedicated plasticising unit and tight scrap control — the material cost does not forgive rejects.
LCP injection-moulded connector

LCP

Liquid crystal polymer

Continuous service temp.

to 240 °C

Walls below 0.3 mm, and dimensions that stay put.

Advantages

  • Extremely low viscosity — fills ultra-thin sections
  • Effectively zero moisture uptake
  • Excellent dielectric performance

Processing challenge

Strongly anisotropic, with markedly weak weld lines. Gate design and position govern part strength, so we resolve them with the tool design rather than after the tool is cut.

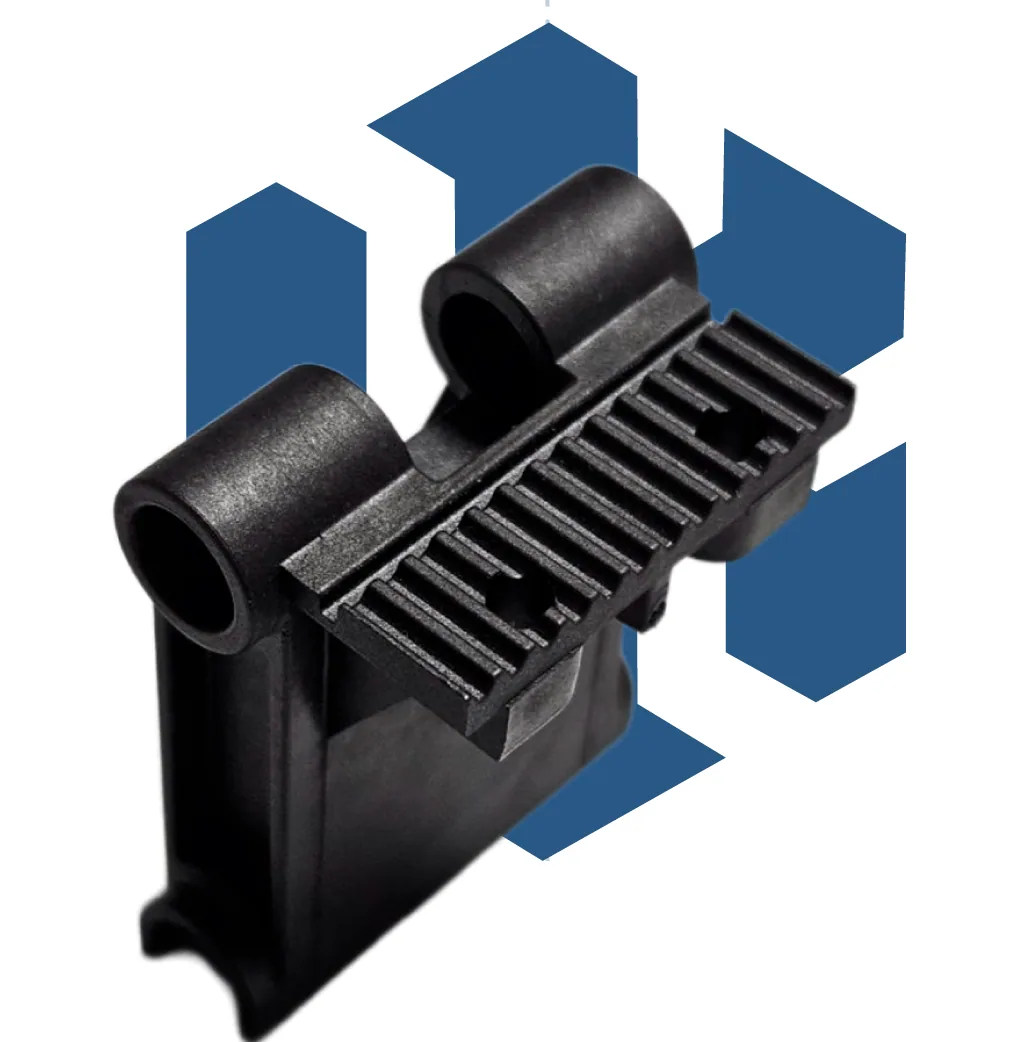
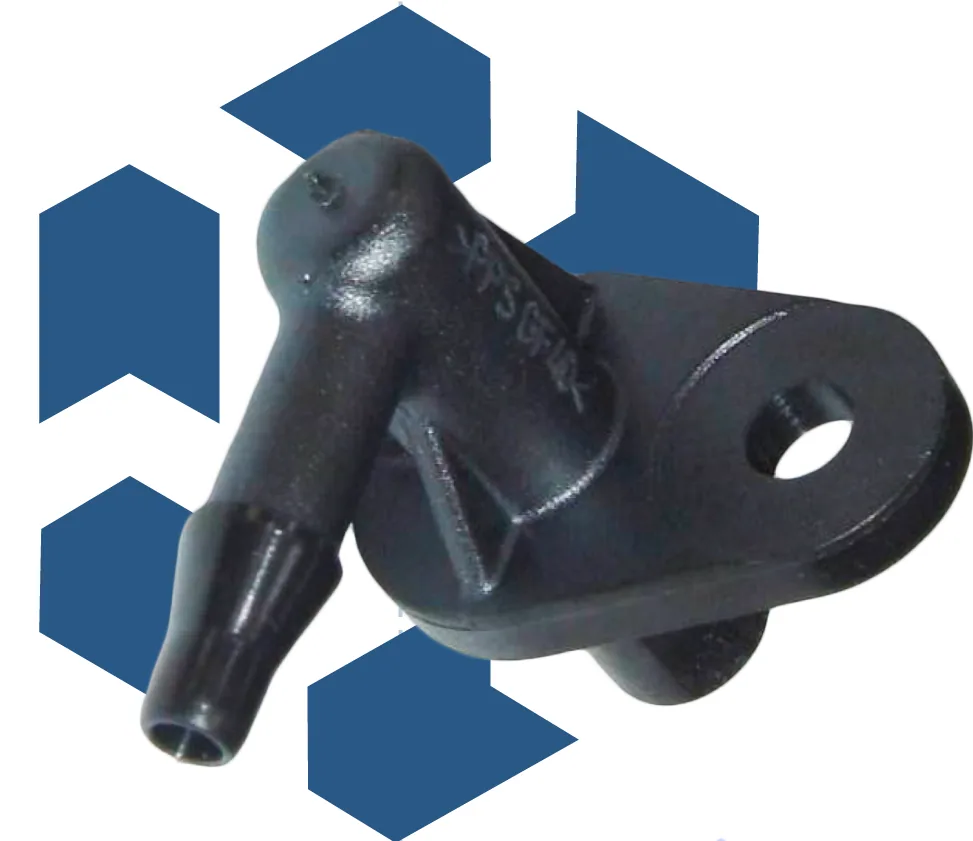
Glass-fibre PPS injection-moulded bracket

PPS

Polyphenylene sulphide

Continuous service temp.

to 220 °C

Chemistry, temperature and dimensional stability at once.

Advantages

  • Chemical resistance approaching PEEK at lower cost
  • Inherently flame retardant without additives
  • Very low dimensional drift in service

Processing challenge

Very low viscosity encourages flash, and glass filling is aggressively abrasive to the tool. We specify higher-hardness tool steels, protective coatings and venting designed for it.

Lubricomp self-lubricating injection-moulded bushing

LNP

Lubricomp — self-lubricating compounds

Continuous service temp.

per base resin

Bearings, gears and slides that run dry.

Advantages

  • Reduced coefficient of friction and wear
  • Removes lubrication from moving assemblies
  • Available on PA, POM, PPS and PEEK bases

Processing challenge

PTFE, silicone and aramid fillers need a gentle plasticising regime so the additive structure survives. We set parameters against the target tribological behaviour, not against cycle time.

Not sure which polymer fits? Our engineers select the material against your design requirements — it is part of how we quote. We also process standard engineering plastics — POM, PA, PC, PBT, PMMA, TPE — to match your project's requirements.

02

Capabilities

Design, tooling, moulding, assembly and logistics on one site. A single partner owns the chain — from flow simulation to despatch.

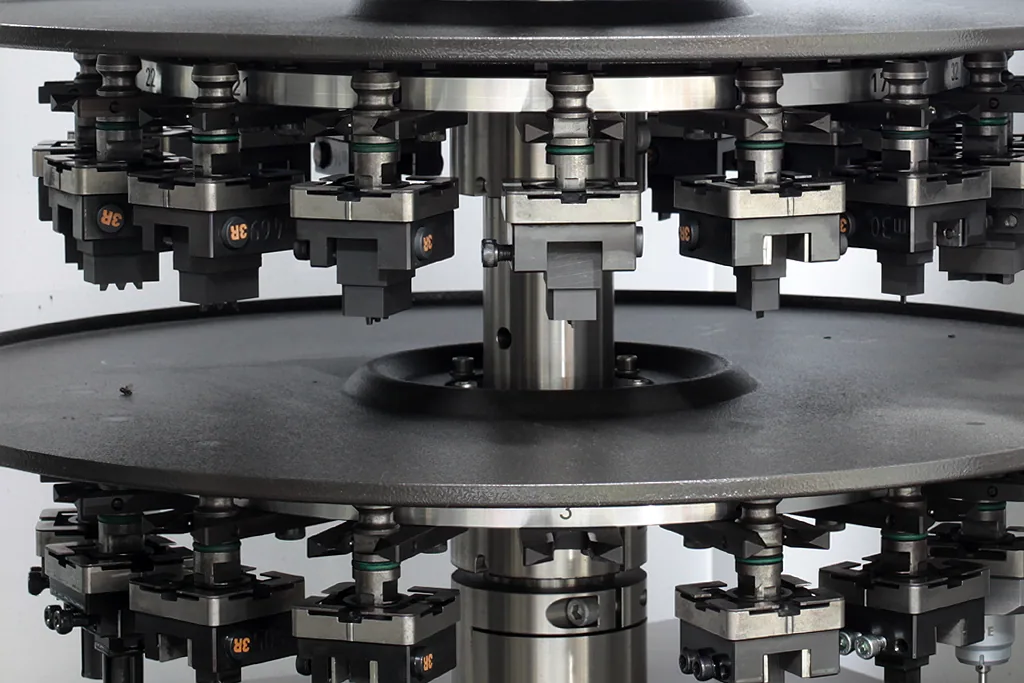
Electrodes in System 3R holders on the EDM tool magazine
A

Toolroom

Injection mould design and build, computer flow analysis, and full tool service throughout series production — with laser repair available around the clock.

  • CAD/CAMCreo · Siemens NX · Solid Edge
  • SimulationCadMould
  • Mould sizeto 600 × 800 mm
  • Mould weightto 2 t
  • Electrode millinggraphite, 3- and 5-axis, unattended
  • Tool repairlaser welding, 24/7
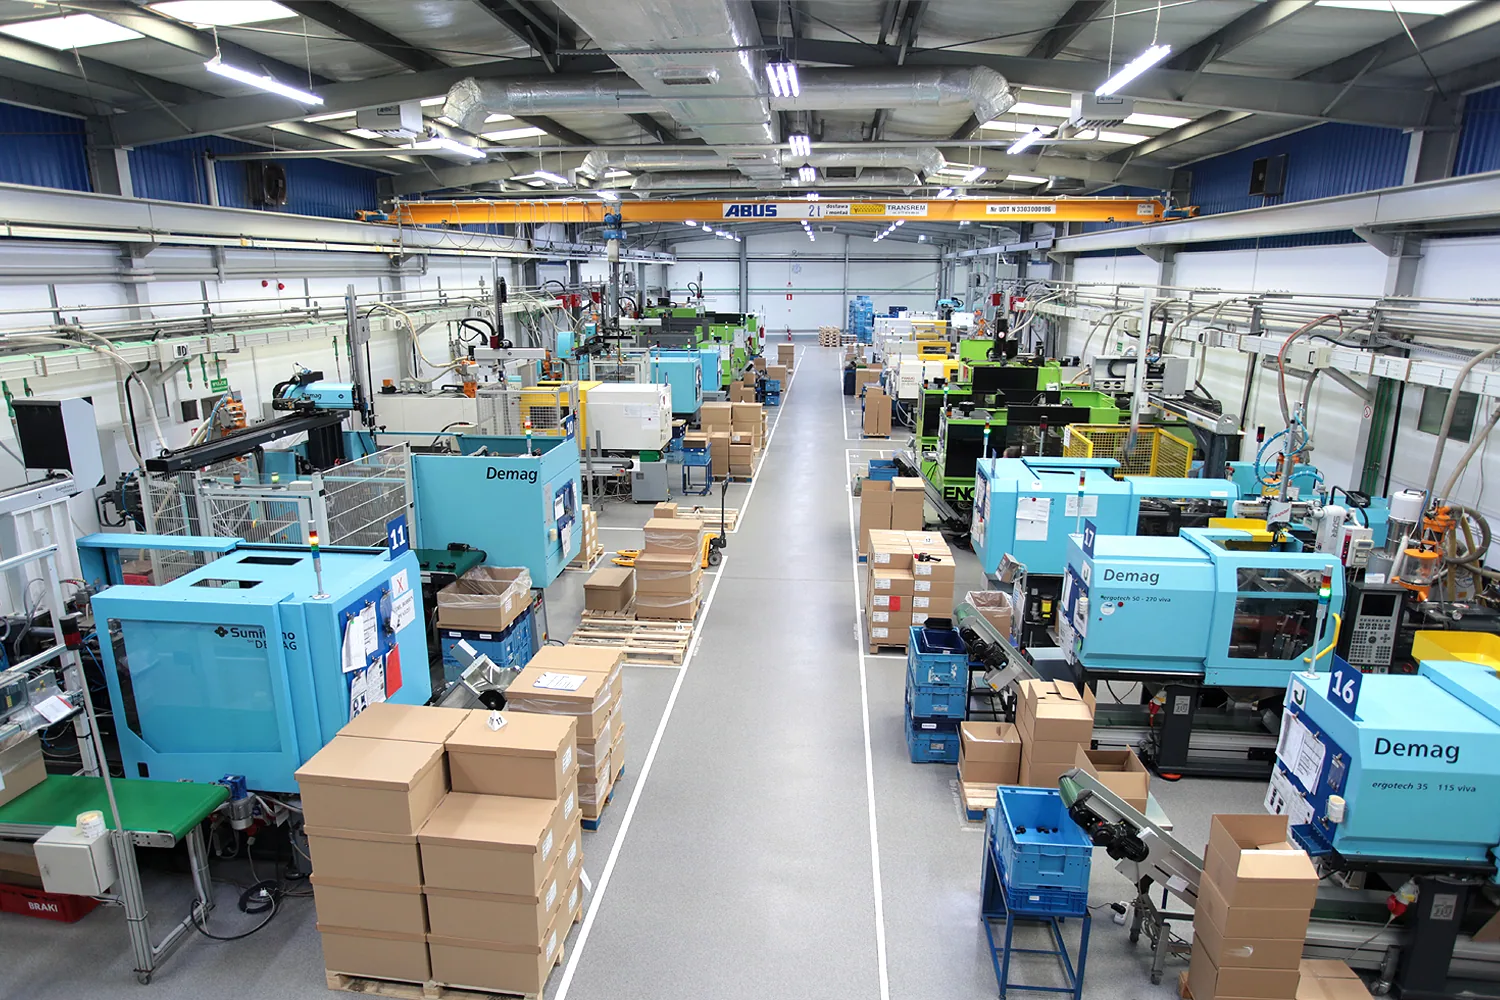
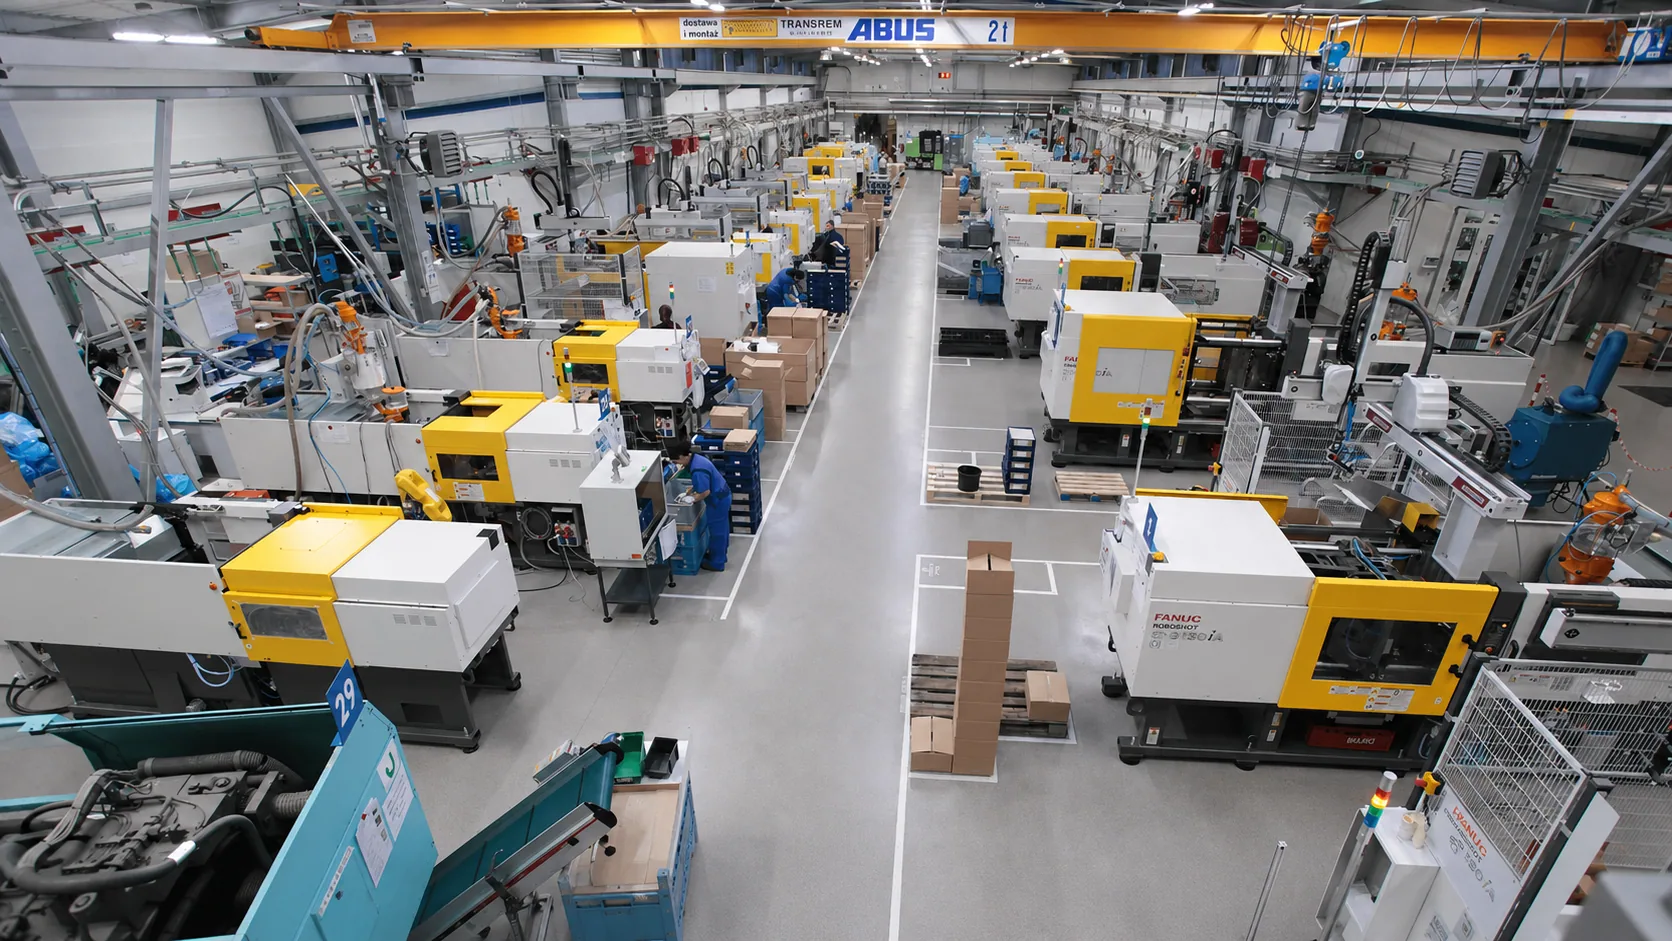
Production hall with automated injection moulding cells
B

Injection moulding

More than 30 injection moulding machines, including 32 automated cells; most machines use electric drives. Robots handle part take-out, insert placement and in-line inspection; the production run is supervised through an MES.

  • Clamping force300–3000 kN
  • Part weight1–500 g
  • MachinesEngel · Demag · Fanuc
  • RobotsWittmann 3-axis · Fanuc 6-axis
  • Feed and dryingKOCH central system
  • SupervisionMES · OEE · OTD
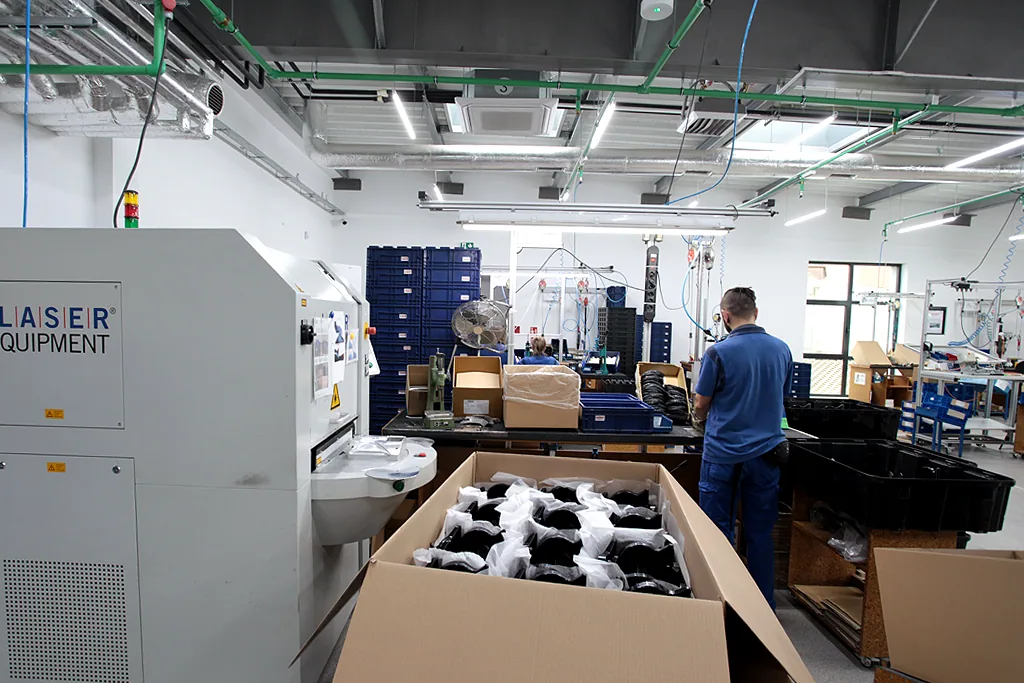
Assembly and laser welding station
C

Assembly & finishing

Ready-to-fit assemblies: mechanical assembly, laser welding and engraving, pad printing, on purpose-built stations designed around the product.

  • Joininglaser welding
  • Markinglaser · pad printing
  • Cleaningultrasonic
  • Stationsproduct-specific
  • Packagingdedicated, shipment-ready
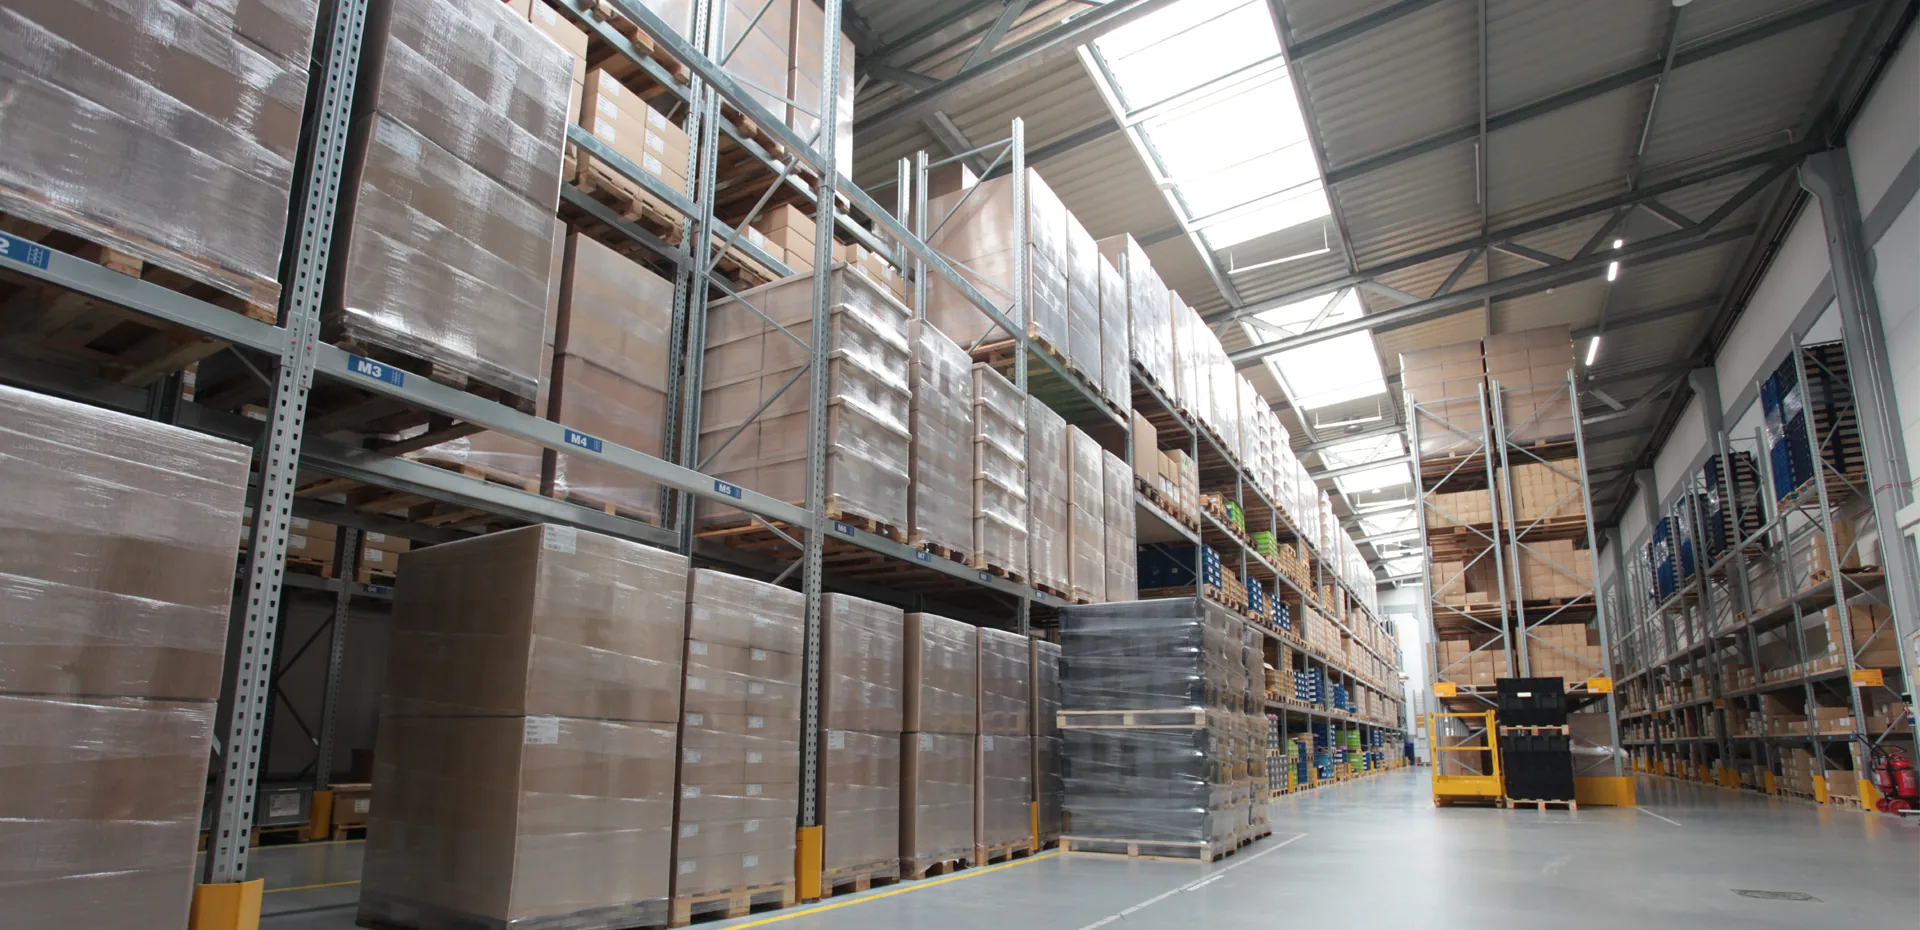
High-bay warehouse
D

Warehouse & logistics

High-bay warehouse under WMS control, with batch identification and delivery to the schedule agreed with you.

  • SystemWMS
  • Traceabilityfull batch control
  • Modeldedicated storage
03

Industries

We supply buyers for whom documentation and repeatability are the entry condition — not an optional extra.

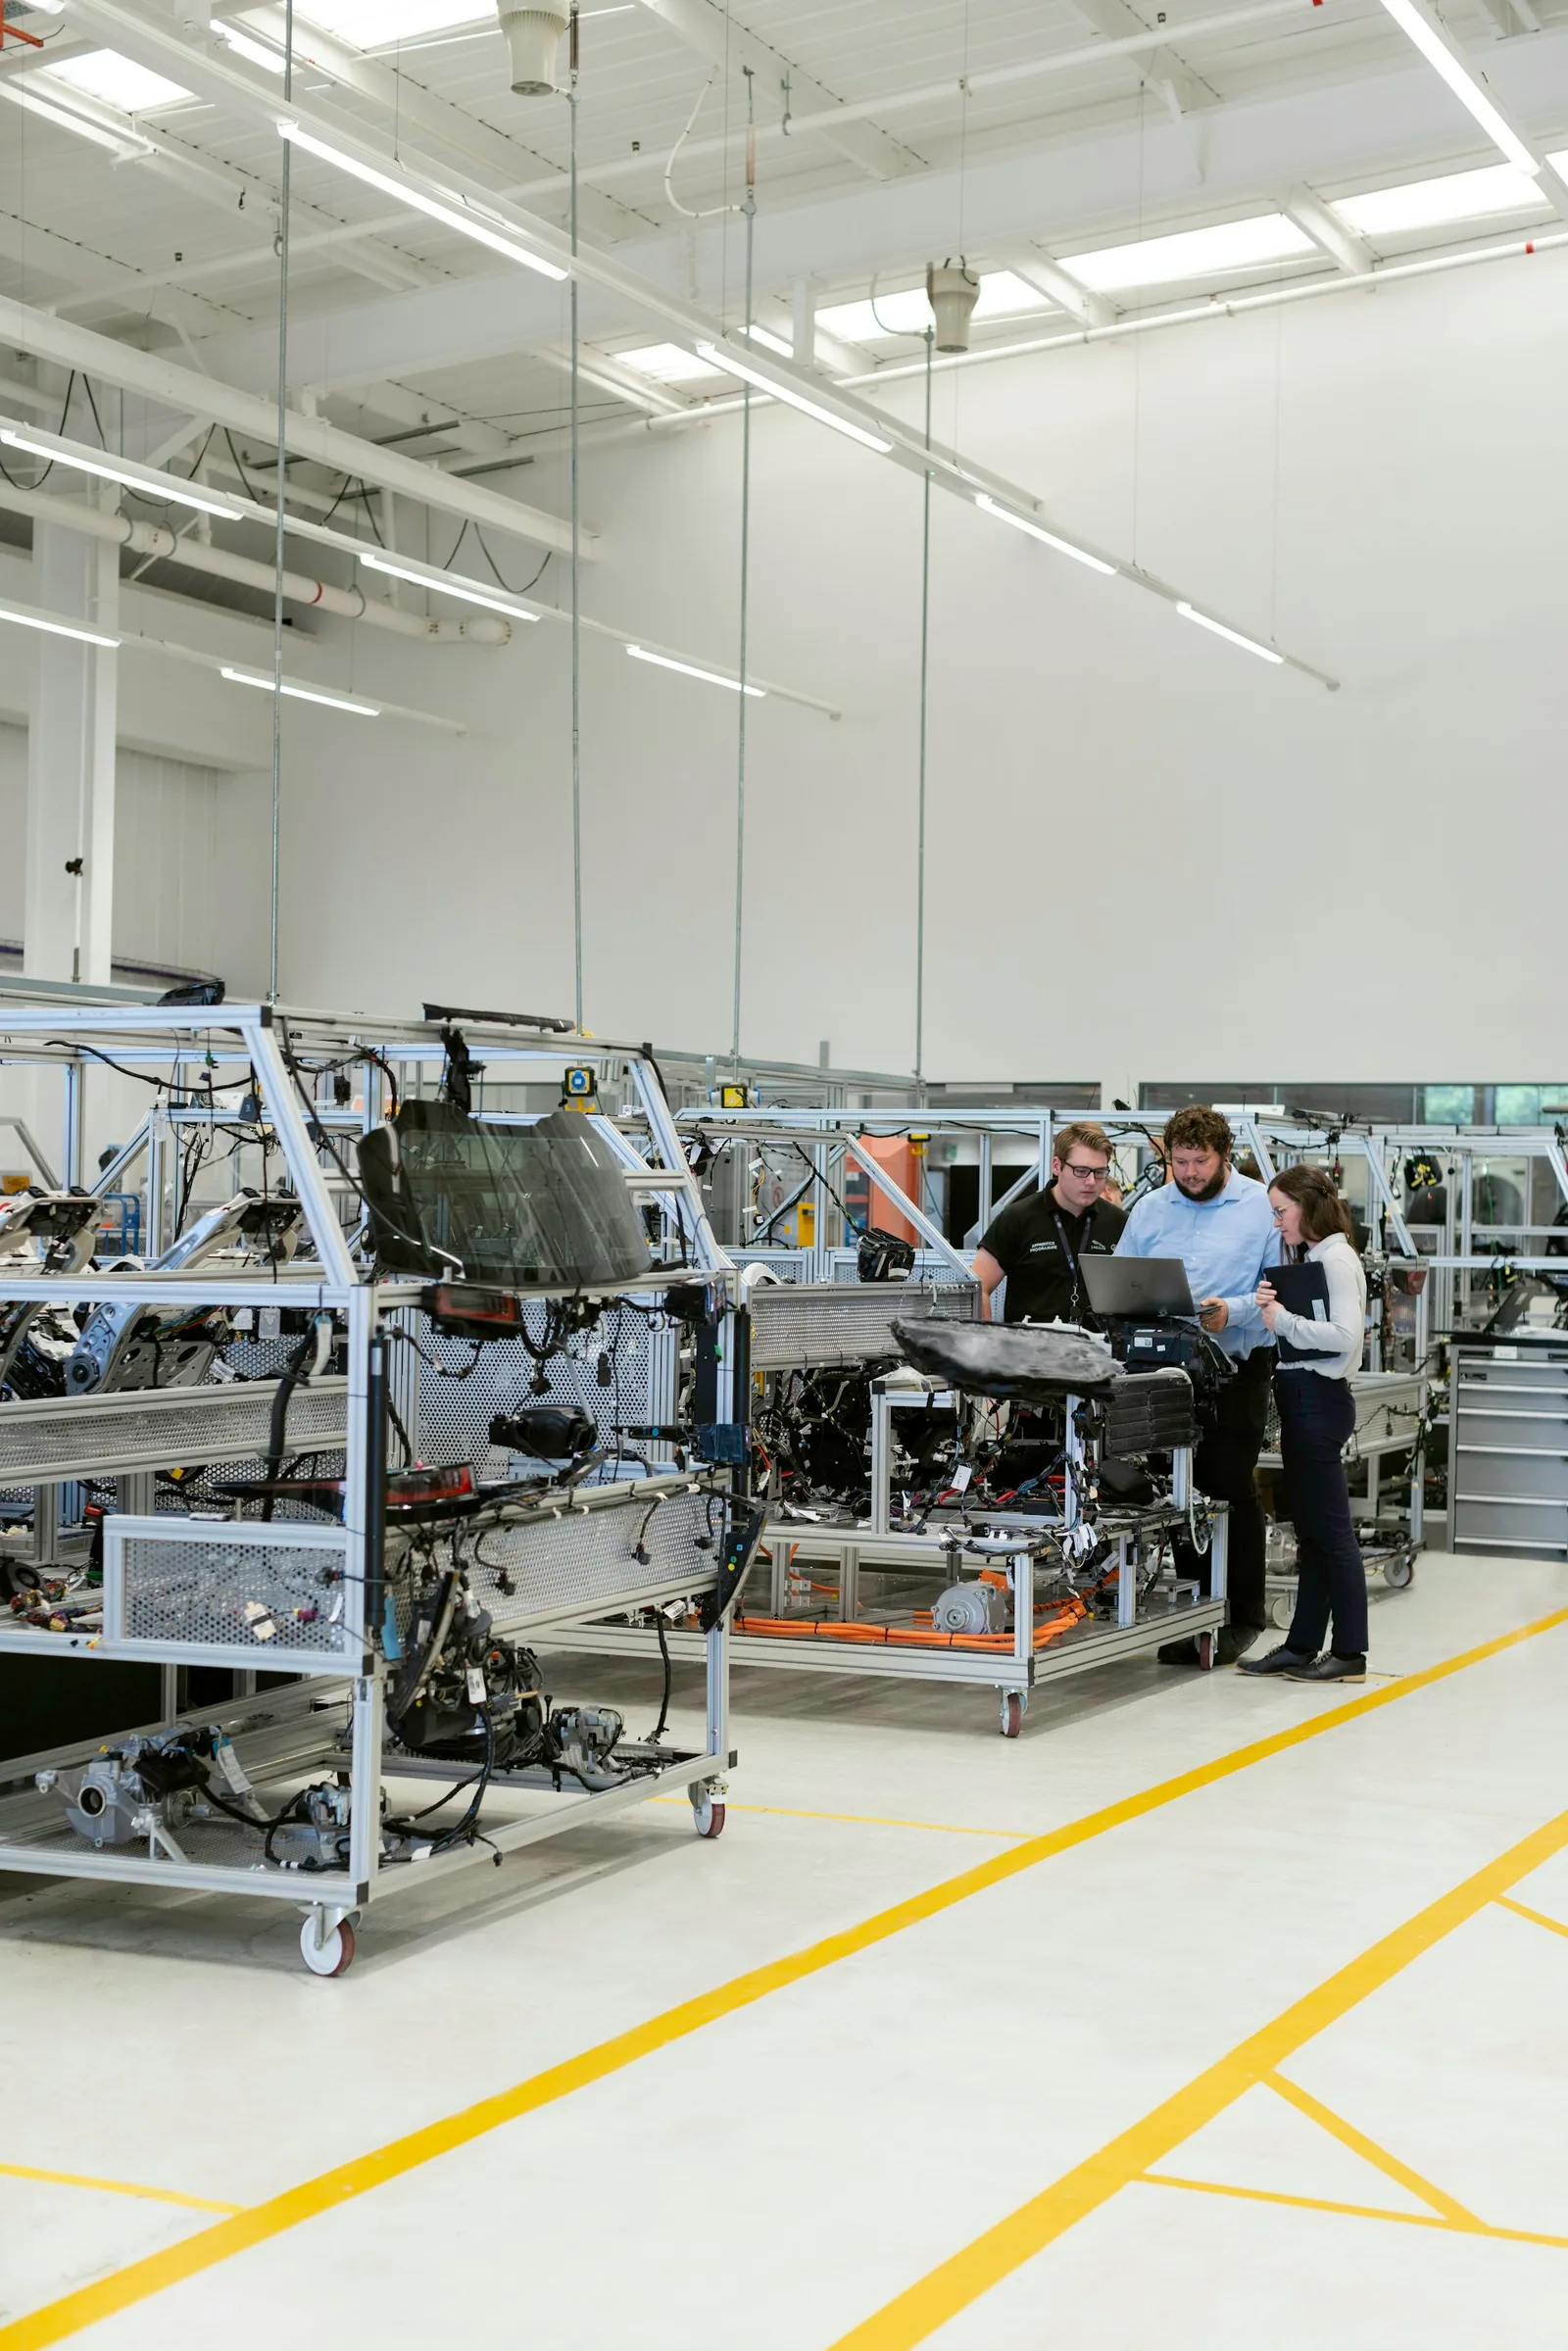
  • Automotive wiring harness assembly line
    01

    Automotive

    Components under IATF 16949, with PPAP documentation and full batch traceability.

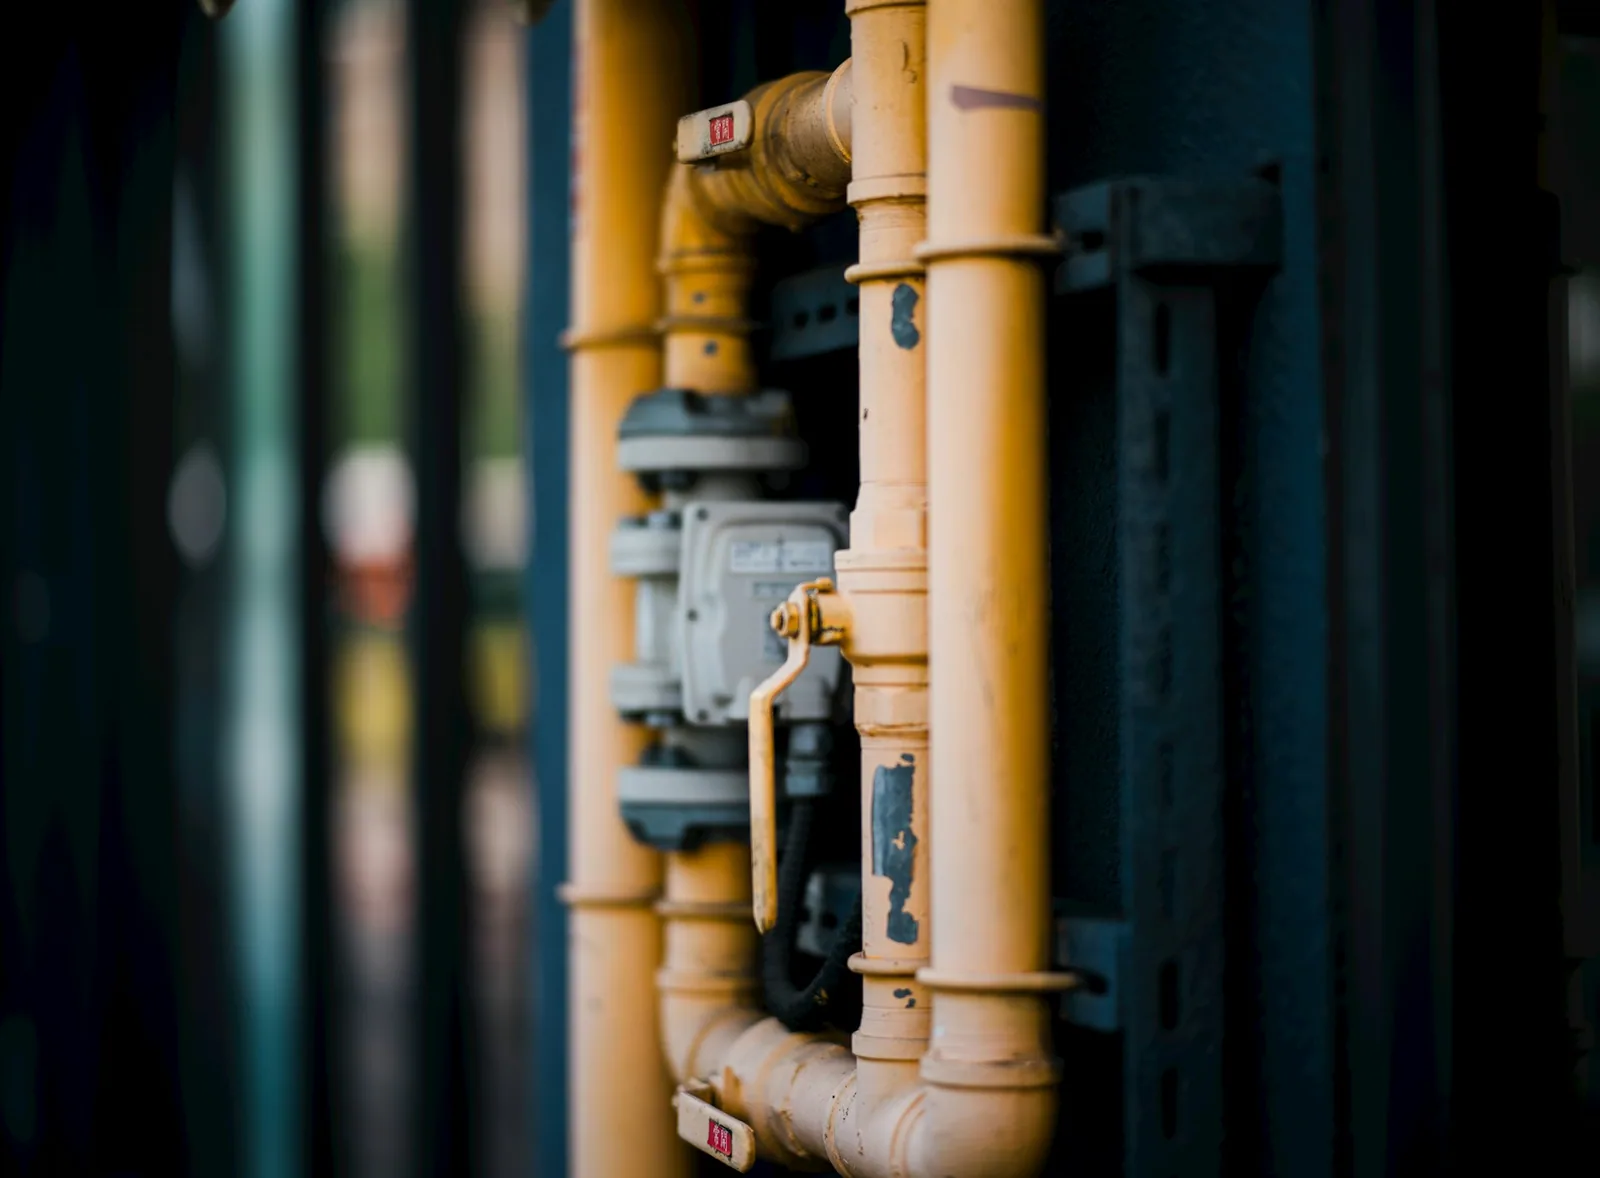
  • Industrial gas piping and valves
    02

    Gas

    Parts with sealing and media-resistance requirements, produced under a controlled process.

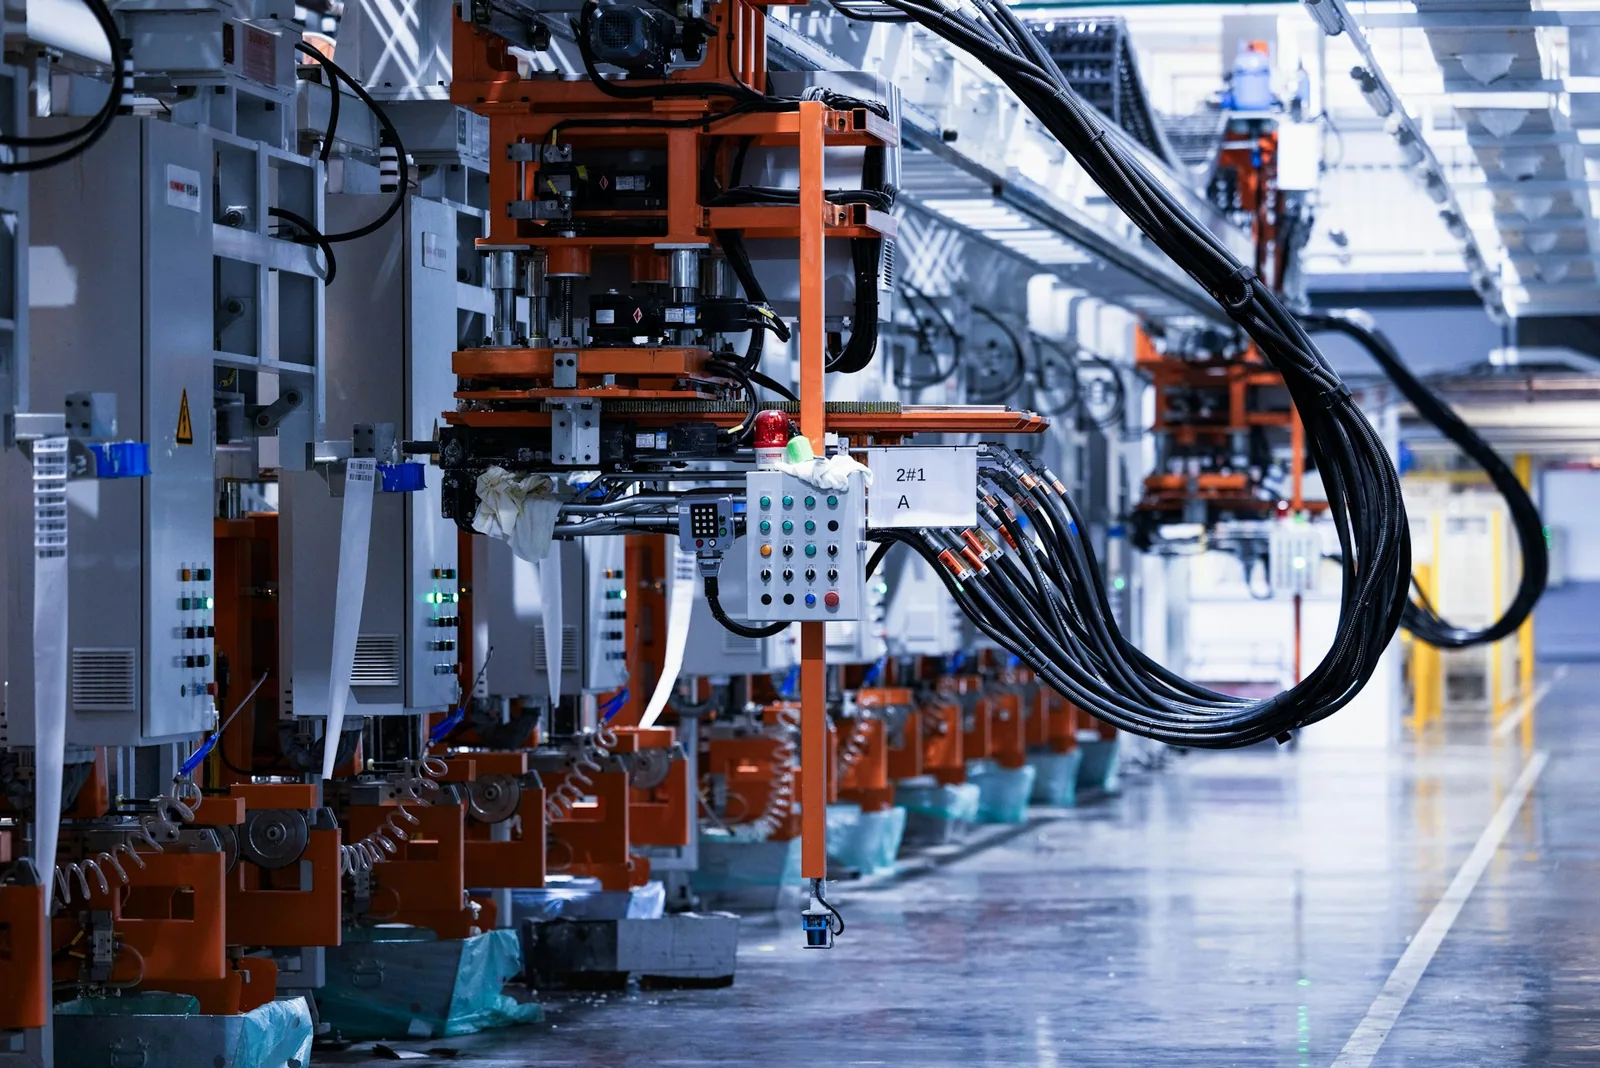
  • Automated electrical/electronics production line
    03

    Electrical engineering

    Dielectric-critical parts and thin-wall housings — core LCP territory.

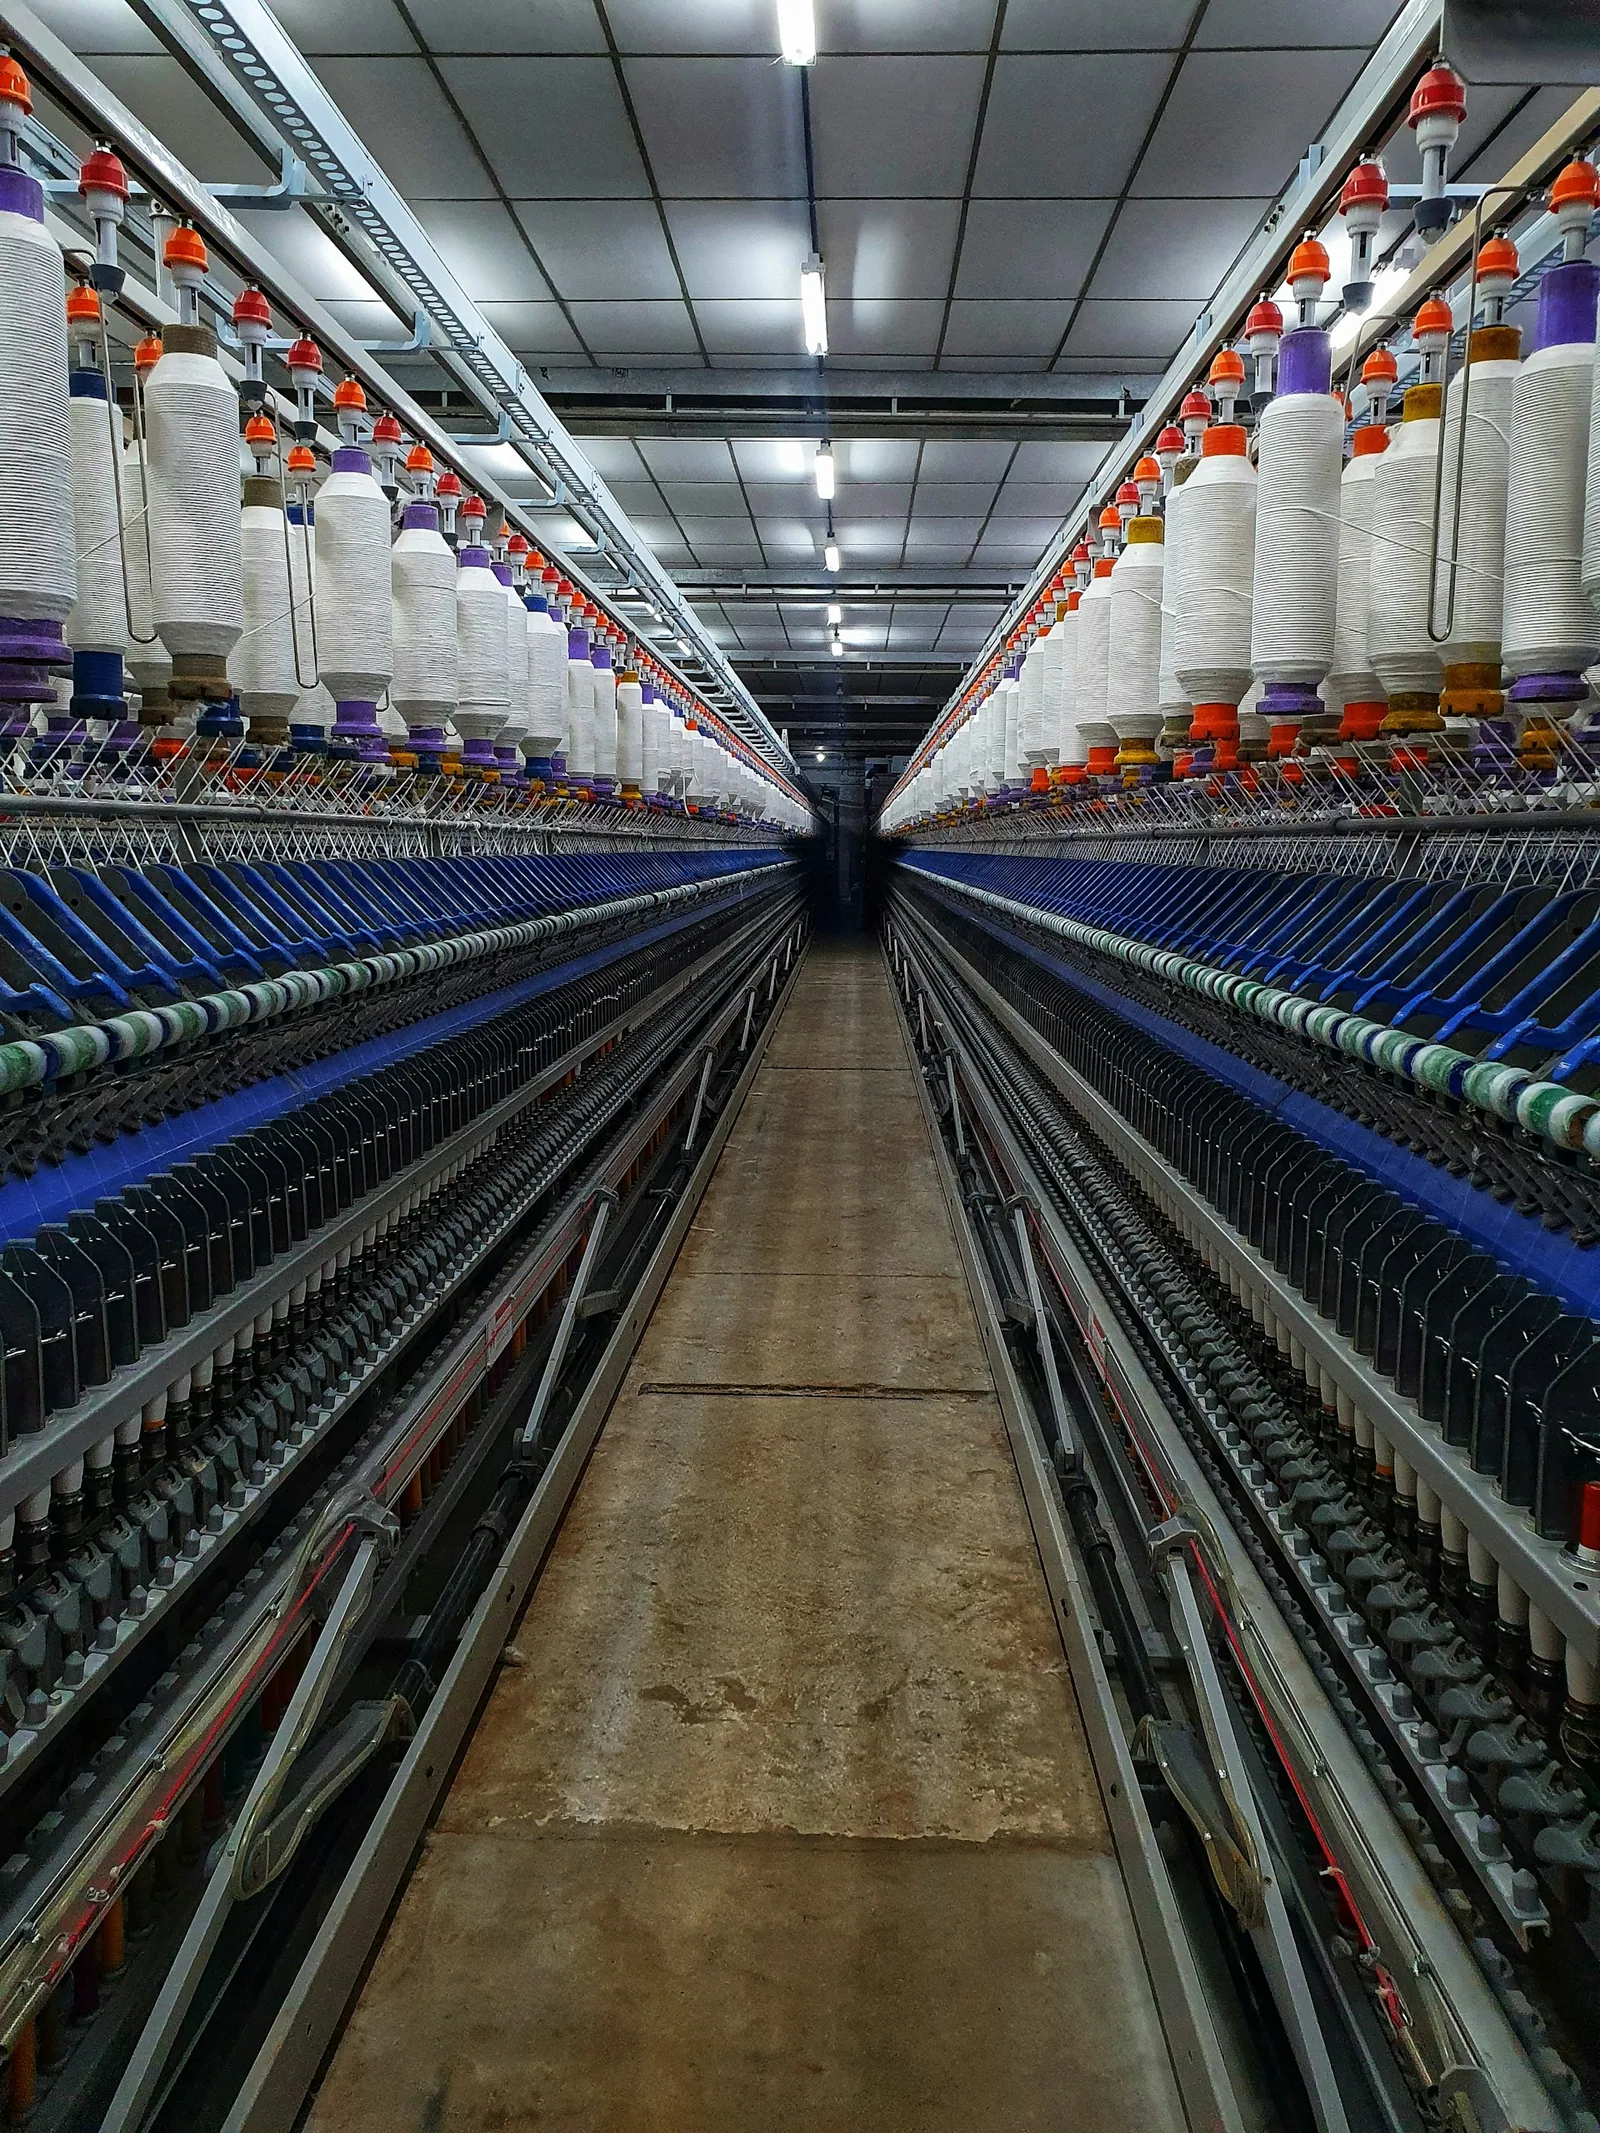
  • Industrial textile spinning mill
    04

    Textile

    High-wear components running continuously without lubrication.

  • Precision-machined metal components
    05

    Machinery

    Gears, guides and sliding elements in self-lubricating compounds.

  • +

    Your industry?

    Not on the list? New applications are business as usual for us — let's talk about your project.

    Request a quote
04

Quality & metrology

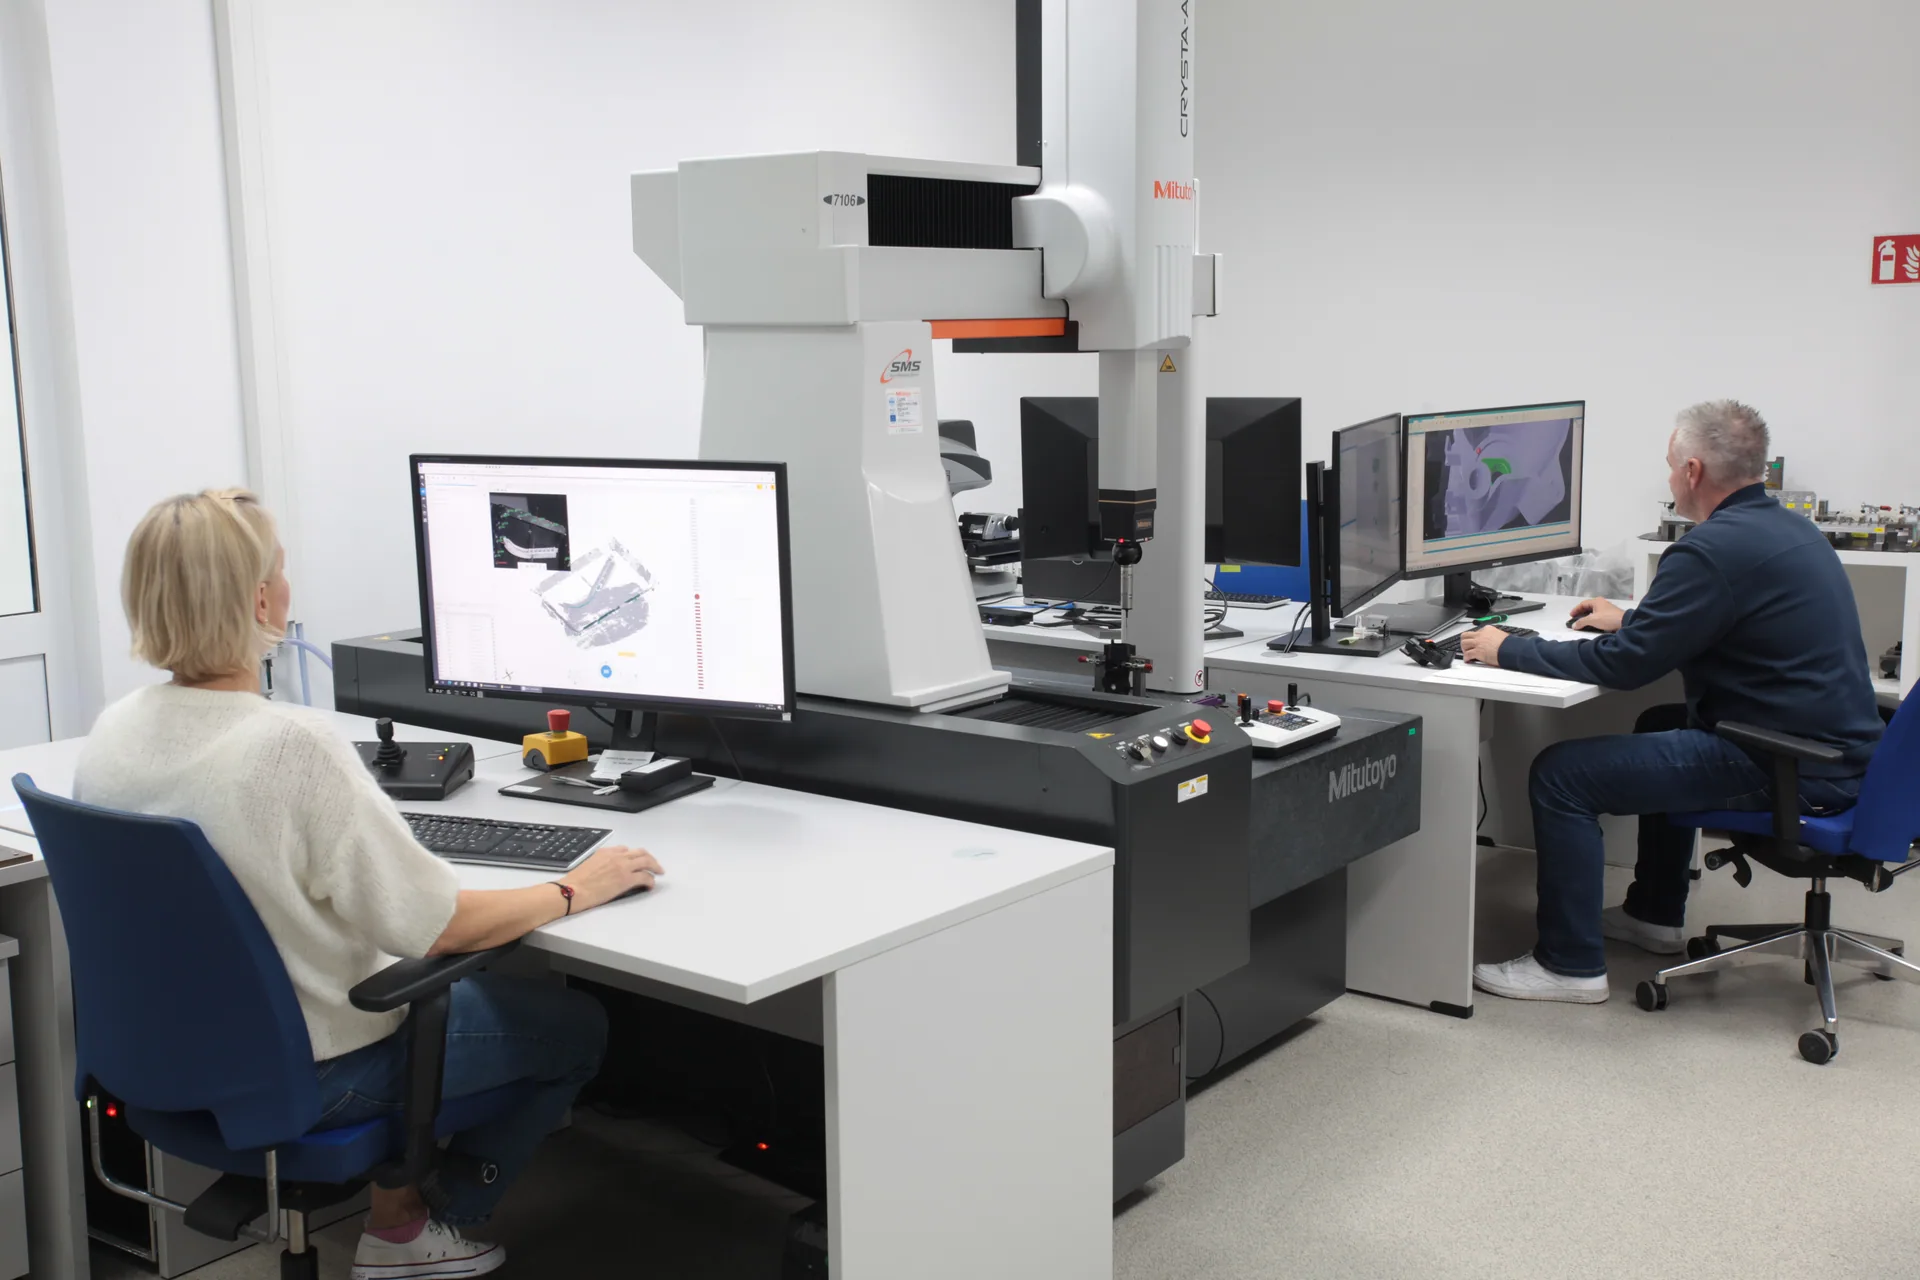
An in-house measuring laboratory, qualified quality engineers, and oversight of both tooling and purchased material — from project start through series production.

Measuring equipment

  • ZeissCoordinate measuring machine
  • MitutoyoCoordinate measuring machine
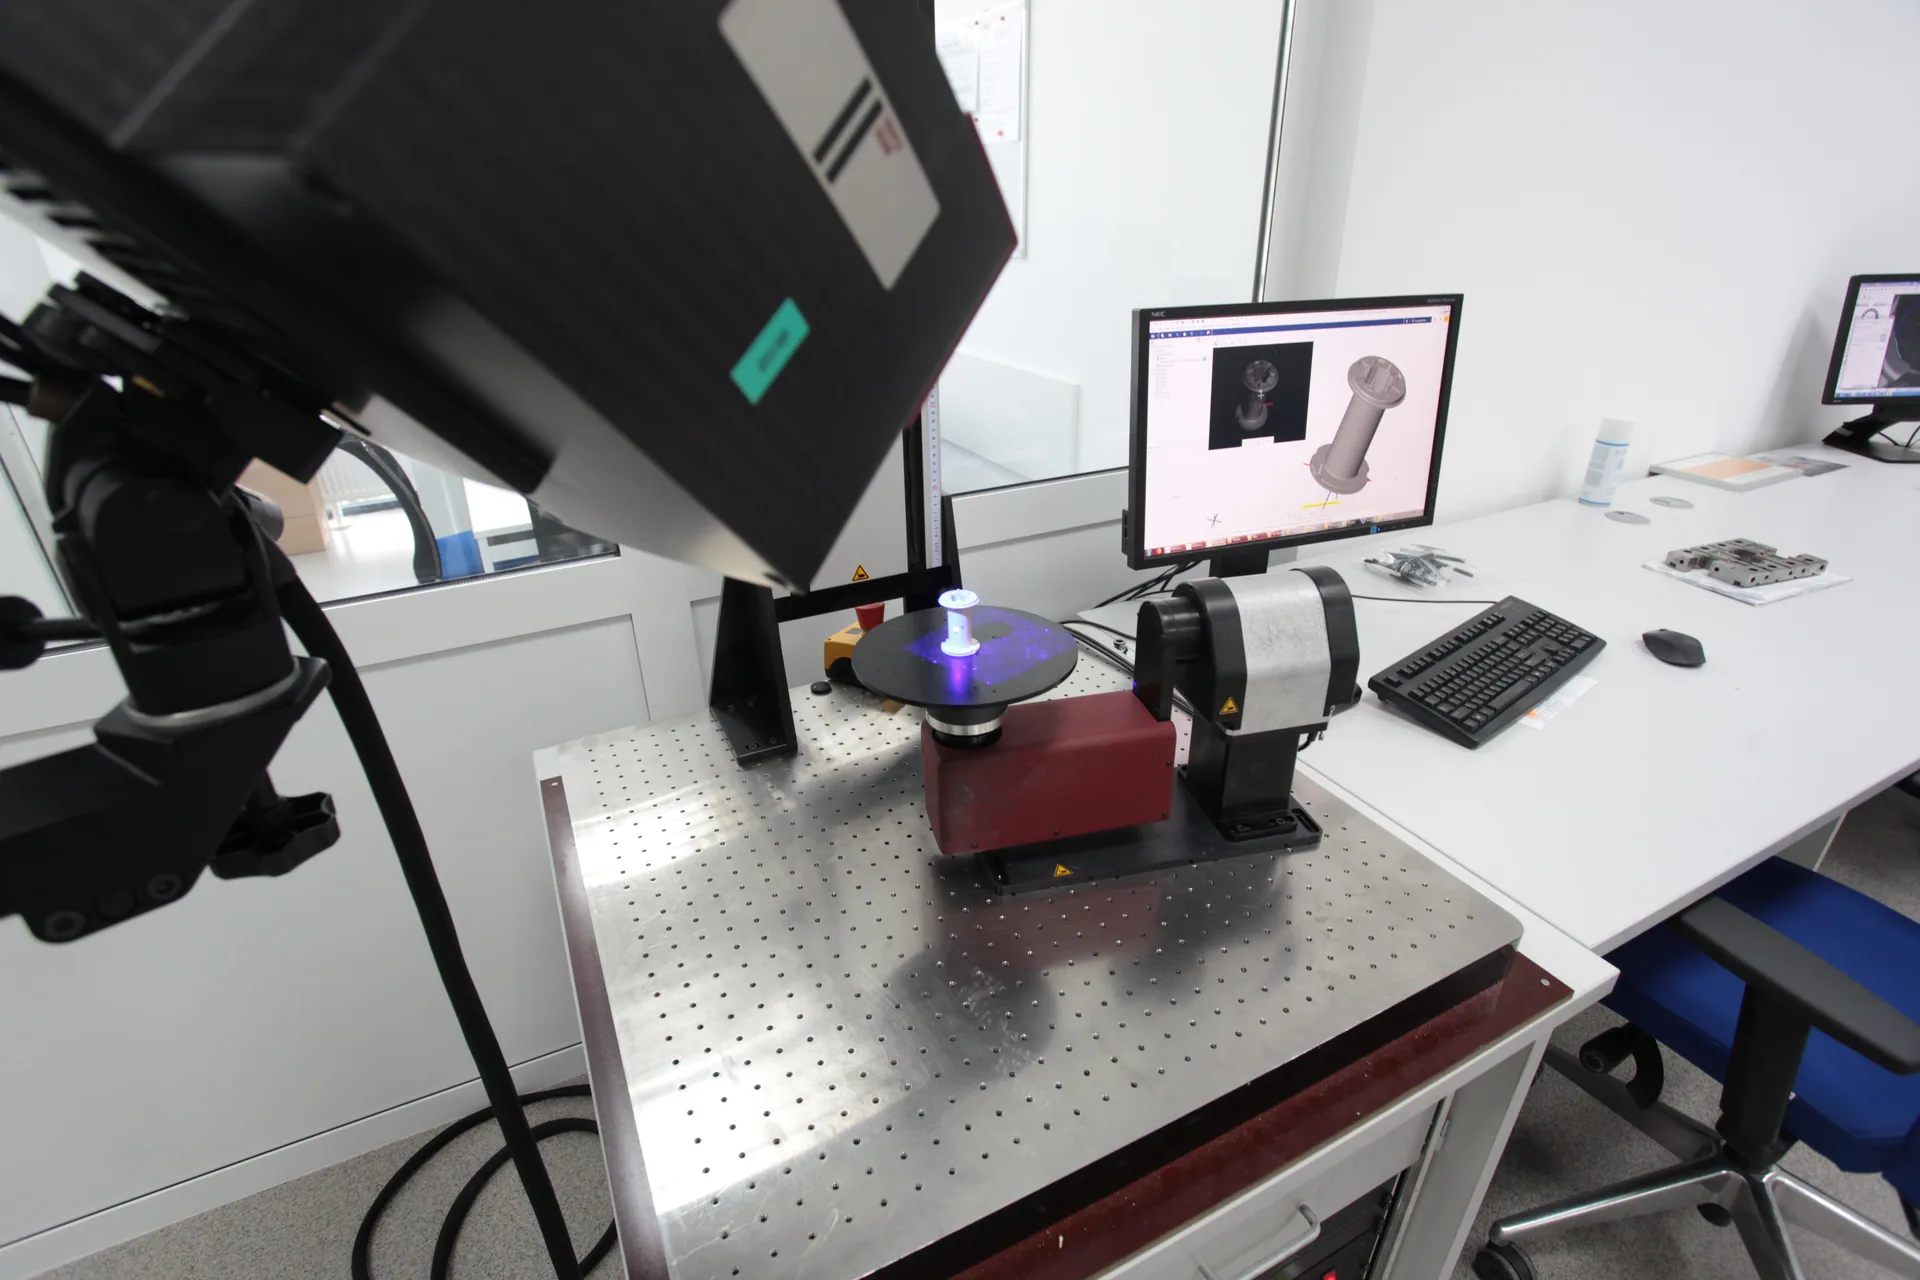
  • GOM3D optical scanner
  • Keyence3D optical profilometer
  • ZeissOptical microscope

Laboratory services

  • Dimensional measurement — length and angle
  • Form and position tolerance analysis
  • Evaluation and interpretation of measurement results
  • Reverse engineering of components
  • 3D scanning

Certification

Mitutoyo coordinate measuring machine in the metrology lab; operators on both sides, with a 3D scan and CAD model on the screens
3D scanner projecting structured light onto a part on a rotary stage, with the scan result visible on the monitor
05

How we run a project

A repeatable path from request to series production. You know what happens at each stage, and where the cost decisions are made.

Milestone definition is what makes project management work. We run on a Plan–Do–Check–Act cycle.

Plan
Do
Check
Act
  1. 01

    Request & feasibility

    We review geometry, material and volume, and flag design risk before any steel is cut.

  2. 02

    DFM & flow simulation

    CadMould analysis of filling, weld lines, shrinkage and warpage. Corrections go into the model, not into a complaint.

  3. 03

    Tool design & build

    Mould designed and built in our own toolroom, against an agreed milestone schedule.

  4. 04

    Sampling & optimisation

    Trials on our own machines, part measurement, and process tuning into a stable production window.

  5. 05

    Approval & PPAP

    Approval documentation to the agreed scope, with measurement reports and control plan.

  6. 06

    Series production & support

    Indicator monitoring, tool servicing and delivery logistics across the product lifecycle.

06

Request a quote

The more you give us up front, the faster you get a real price instead of follow-up questions. Attach a drawing or 3D model.

Send your request

We respond within 2 working days. Your data and drawings stay confidential.